Pallet Shuttle Upgrade Improves Warehouse Flow for a Leading Food & Beverage Manufacturer in West Africa
Enhancing Existing High-Density Storage with RF Pallet Shuttle Technology
When a Leading Food & Beverage manufacturer in West Africa required a more efficient way to improve pallet movement within its existing high-density warehouse, the company partnered with Logistics Systems Engineering (LSE) to supply and commission advanced Radio Frequency (RF) Pallet Shuttle Technology.
Rather than replacing the existing storage infrastructure, LSE integrated Six RF Pallet Shuttle Units into the customer’s warehouse, providing a cost-effective solution to improve stock flow, reduce forklift travel and increase pallet handling efficiency.
The project was successfully completed within two days, including system commissioning, operator training and handover.
About the Customers
Our customer is one of West Africa’s leading Food & Beverage Manufacturers, operating a high-volume distribution facility that supports continuous production and product movement throughout the region.
With increasing warehouse activity and growing demand, the business required a solution that could improve pallet handling efficiency while making full use of its existing storage infrastructure.
For confidentiality reasons, the customer’s name has been withheld.
The Challenge: Increasing Storage Capacity While Improving Stock Flow
As warehouse demand increased, Wheel Assemblers required a storage solution capable of supporting continued operational growth while making better use of the available warehouse space.
The project objectives included:
- Increasing storage capacity within the existing warehouse footprint.
- Improving stock flow and pallet movement.
- Reducing forklift travel inside storage lanes.
- Supporting high-density storage for large quantities of similar products.
- Improving warehouse productivity and operational efficiency.
- Providing flexible inventory management using both FIFO and LIFO principles.
- Delivering a reliable system suitable for daily high-volume operations.
The customer required a solution that would improve both storage density and warehouse performance without disrupting ongoing operations.
The Solution: RF Pallet Shuttle Integration by LSE
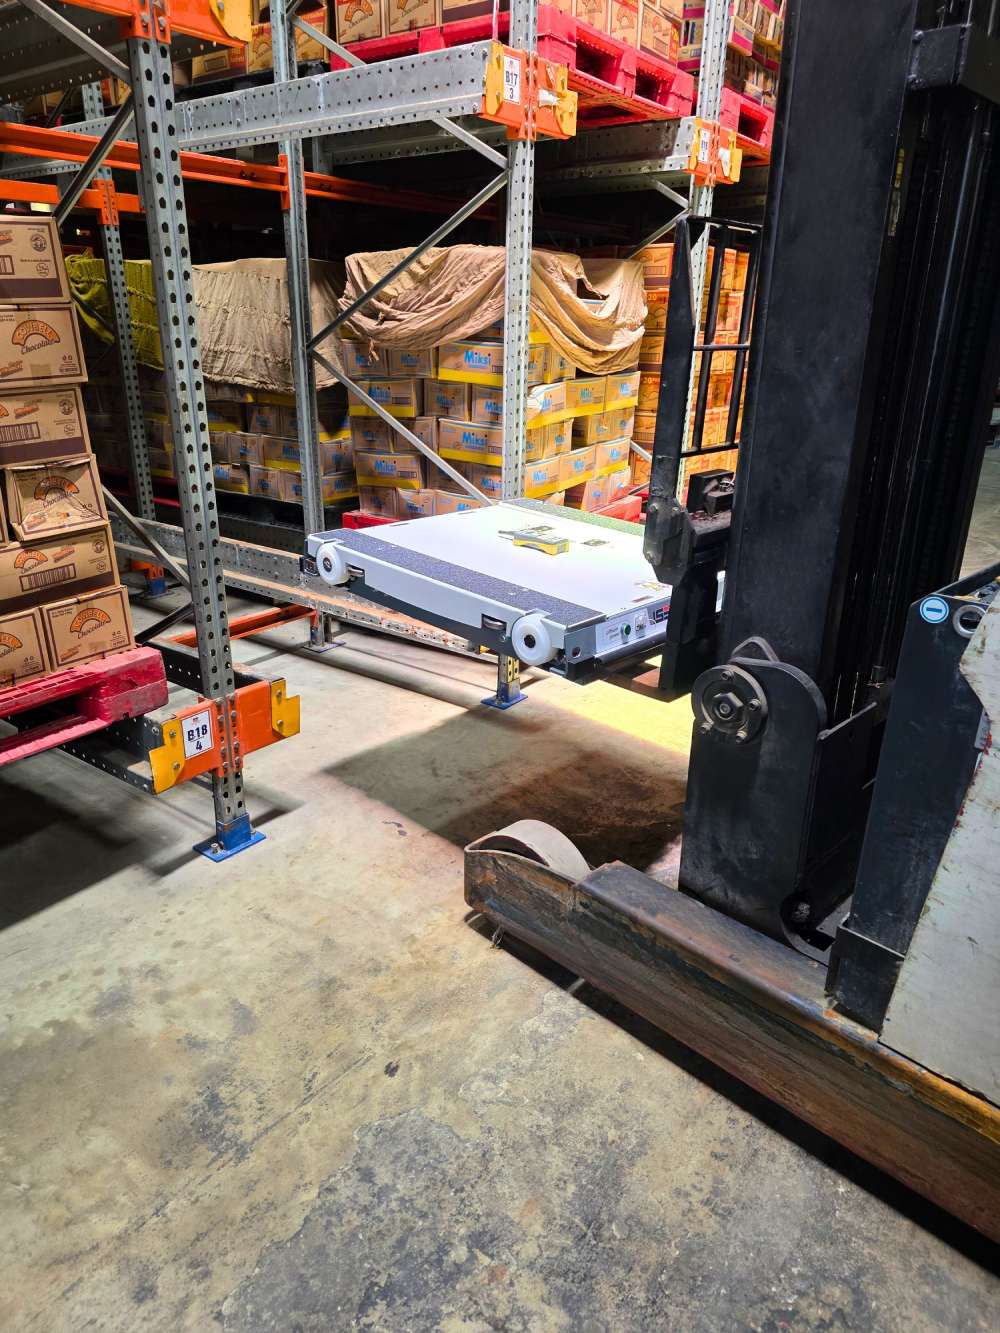
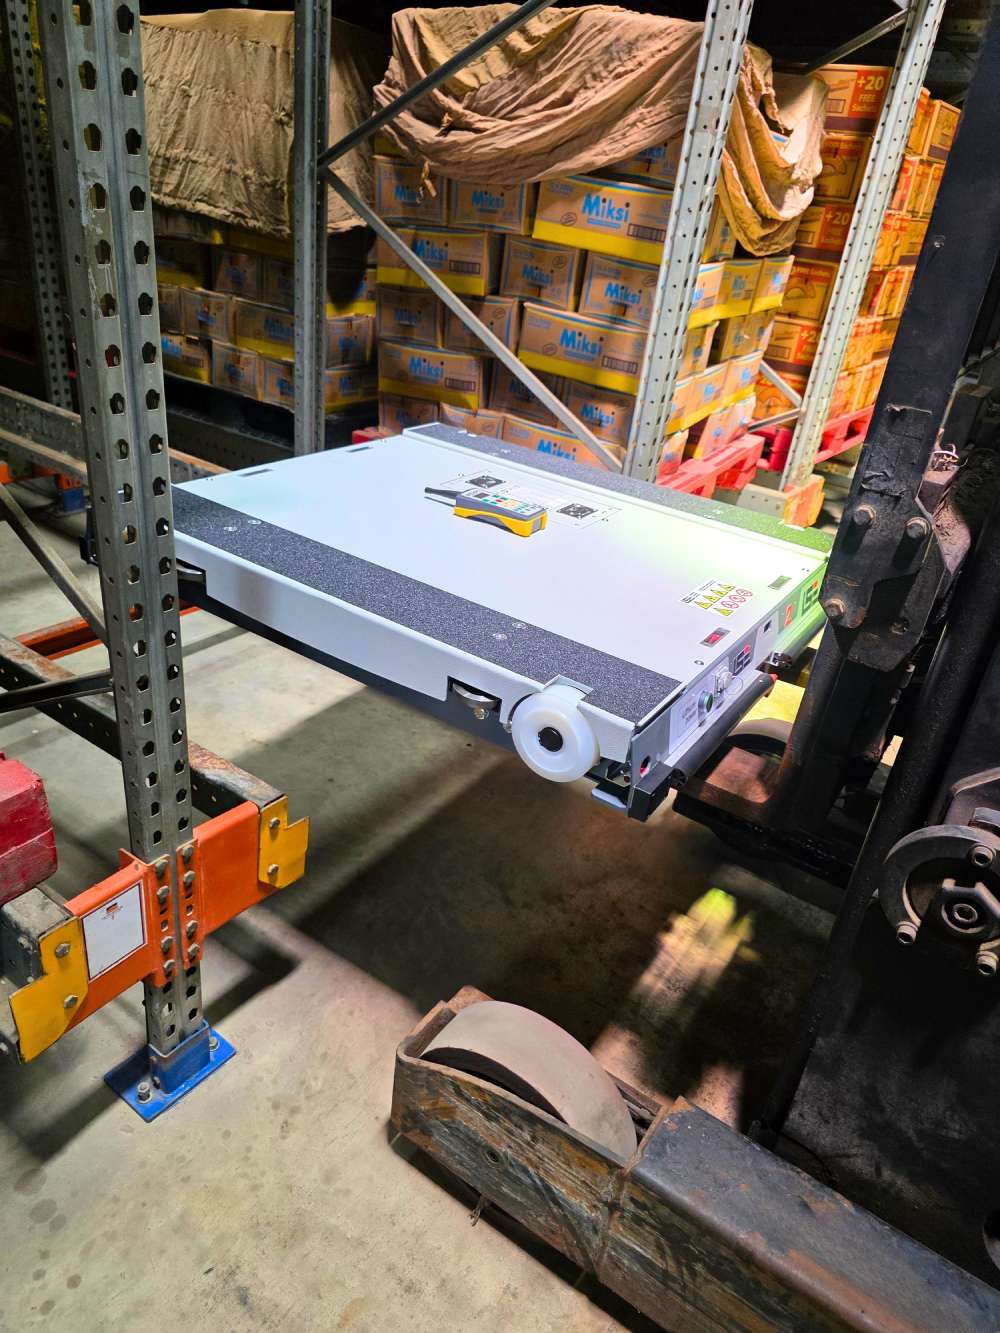
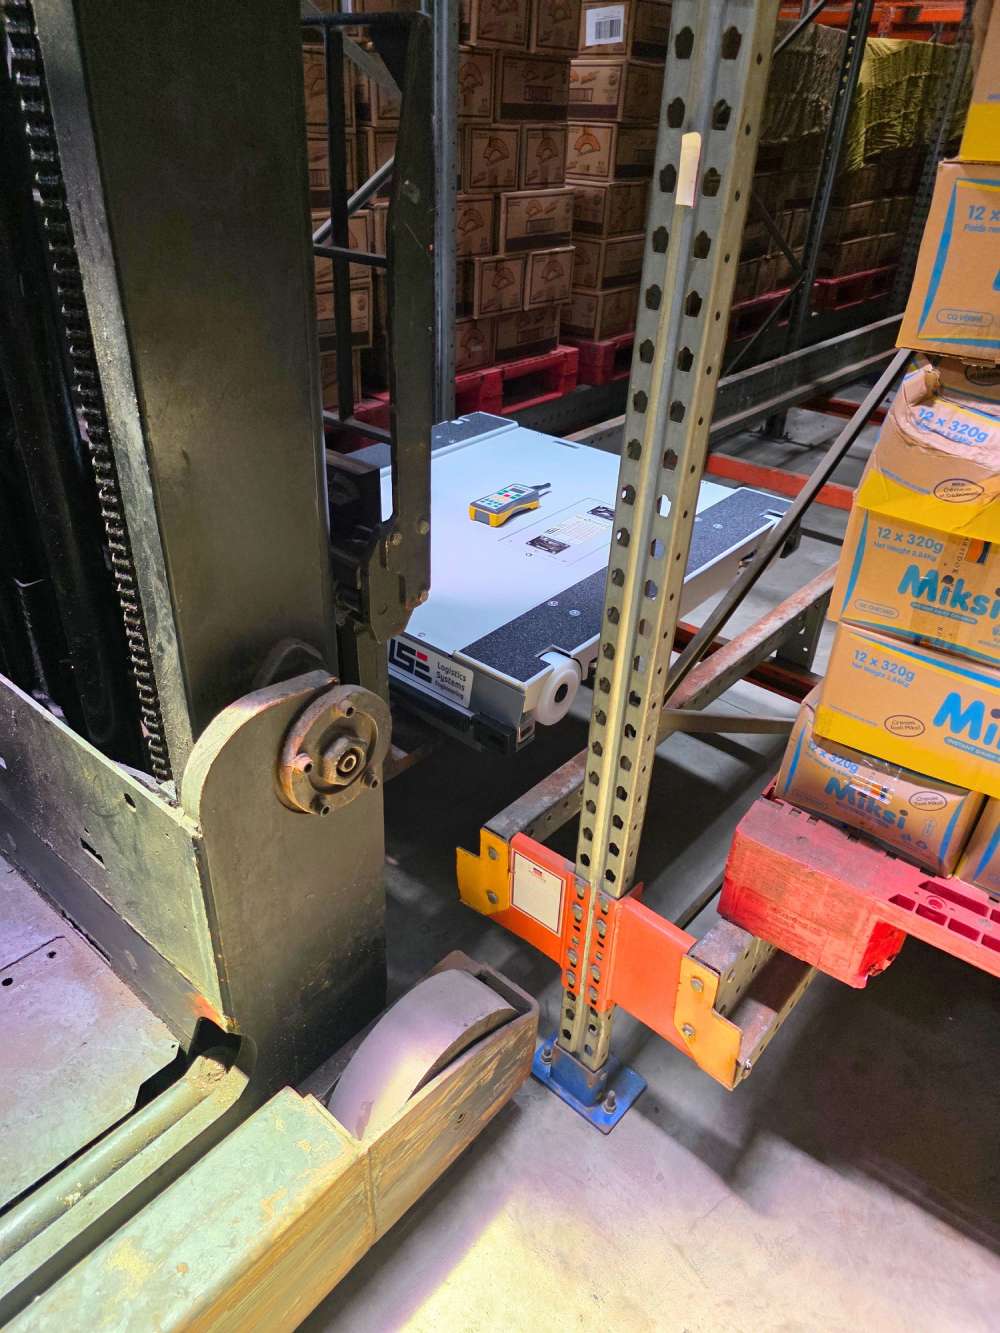
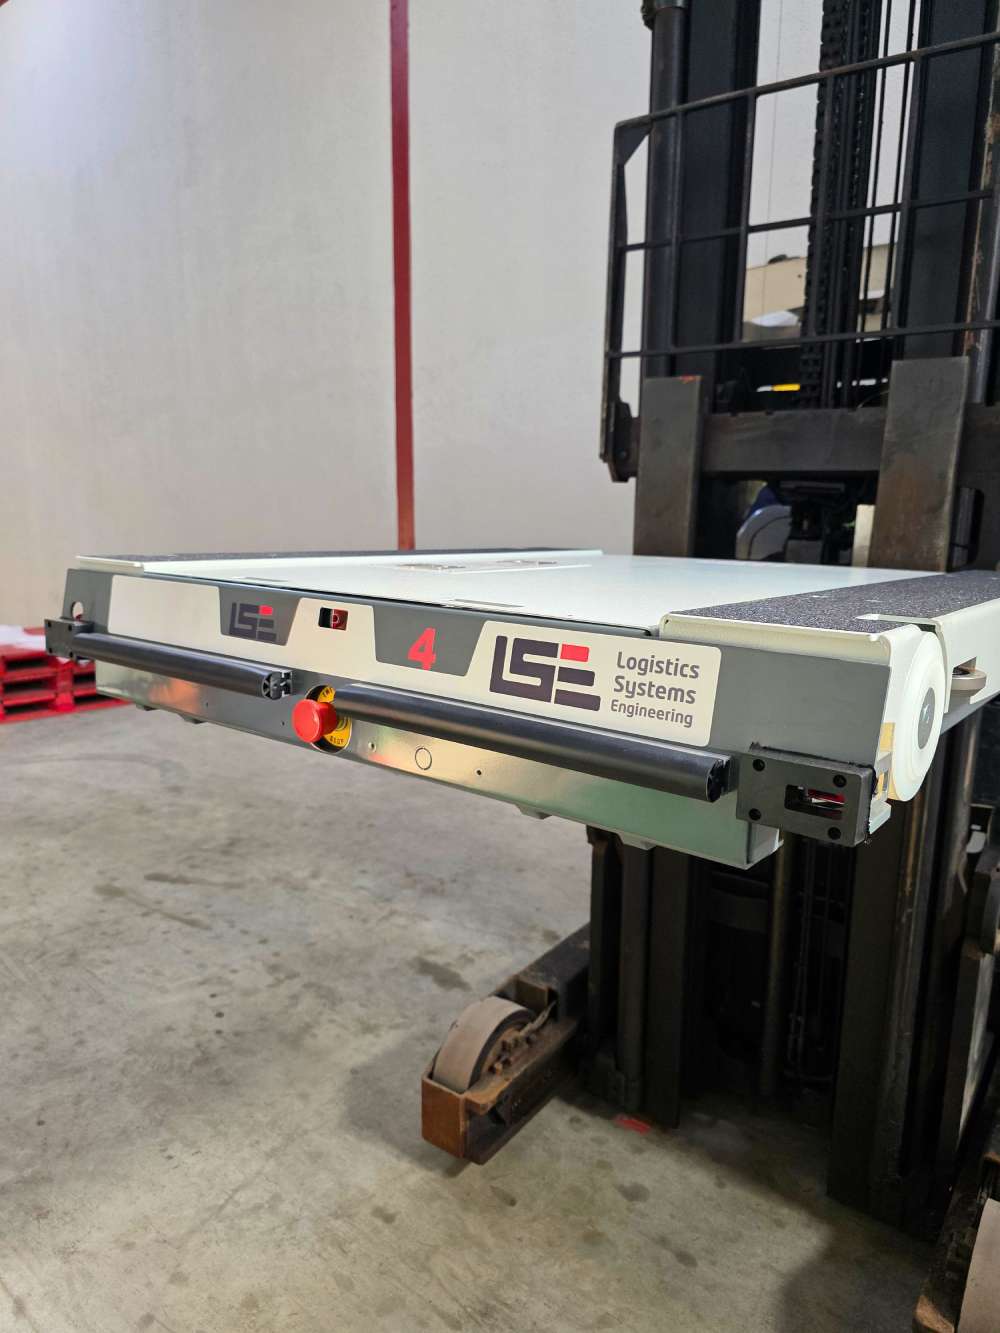
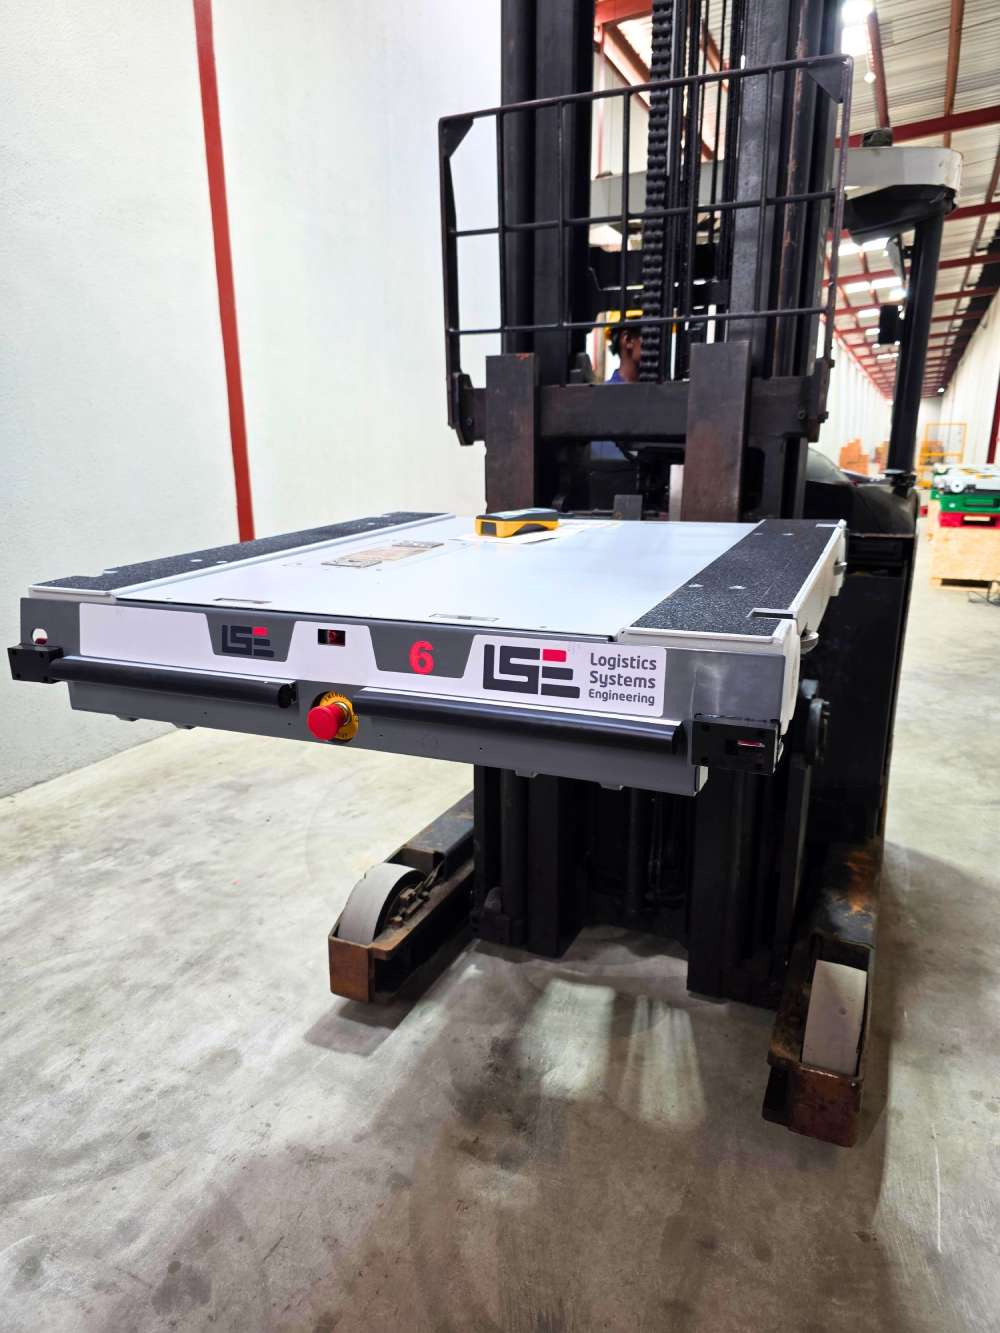
To improve warehouse productivity without replacing the customer’s existing storage infrastructure, Logistics Systems Engineering (LSE) supplied, commissioned and integrated Six RF-controlled Pallet Shuttle units into the customer’s high-density racking system.
Rather than investing in an entirely new warehouse solution, the customer enhanced its existing storage operation with Pallet Shuttle technology, enabling faster pallet movement, reduced forklift travel within storage lanes and improved stock flow throughout the facility.
The RF-controlled Pallet Shuttle System allows operators to remotely transport pallets through deep storage channels, increasing operational efficiency while maintaining a safe and reliable warehouse environment.
Following commissioning, LSE provided comprehensive operator training to ensure the customer’s warehouse personnel could confidently operate the new system safely and efficiently from day one.
Technical Data: RF Pallet Shuttle Integration Project
Pallet Shuttle System
| Technical Specification | Project Detail |
|---|---|
| Industry | Food & Beverage Manufacturing |
| Storage System | Existing High-Density Storage with RF Pallet Shuttle Integration |
| Shuttle Type | RF Pallet Shuttle |
| Number of Shuttles | 6 Shuttles |
| Maximum Pallet Weight | 1 000kg |
| Operating Temperature | Ambient |
| Inventory Management | LIFO |
| Control System | Remote Control |
| Application | Ambient Distribution |
| Project Duration | 2 Days |
Technical Data: RF Pallet Shuttle Integration Project
Pallet Shuttle System
| Technical Specification | Project Detail |
|---|---|
| Industry | Food & Beverage Manufacturing |
| Storage System | Existing High-Density Storage with RF Pallet Shuttle Integration |
| Shuttle Type | RF Pallet Shuttle |
| Number of Shuttles | 6 Shuttles |
| Maximum Pallet Weight | 1 000kg |
| Operating Temperature | Ambient |
| Inventory Management | LIFO |
| Control System | Remote Control |
| Application | Ambient Distribution |
| Project Duration | 2 Days |
Rapid Delivery, Commissioning & Operator Training
The project was successfully completed within two days, allowing the customer to begin benefiting from the new Pallet Shuttle technology with minimal disruption to ongoing warehouse operations.
The project included:
Phase 1 – Project Assessment
LSE evaluated the customer’s existing high-density storage system to ensure compatibility with the RF Pallet Shuttle solution and prepared the equipment for commissioning.
Phase 2 – Shuttle Commissioning
The six RF Pallet Shuttle units were configured, tested and commissioned to integrate seamlessly with the customer’s existing warehouse operation.
Phase 3 – Operator Training & System Handover
LSE conducted comprehensive operator training covering safe equipment operation, remote-control functions, routine operating procedures and best practices, ensuring the warehouse team could confidently operate the Pallet Shuttle System from day one.
Results: Improved Warehouse Performance Without Replacing Existing Infrastructure
The RF Pallet Shuttle integration delivered several immediate operational benefits:
- Improved pallet flow throughout the warehouse.
- Reduced forklift travel within storage channels
- Faster pallet storage and retrieval operations.
- Enhanced utilisation of the existing high-density storage system.
- Cost-effective warehouse upgrade without replacing existing racking.
- Rapid commissioning and implementation within two days.
- Comprehensive operator training for safe and efficient day-to-day operation.
- Increased flexibility to support future warehouse growth and operational improvements.
Customer Handover
Following successful commissioning, LSE completed a full system handover, ensuring the customer was fully equipped to operate and maintain the RF Pallet Shuttle System.
The handover included practical operator training, system familiarisation and operational guidance, enabling the warehouse team to maximise the benefits of the new technology from the outset.
This project demonstrates LSE’s ability not only to deliver complete high-density storage solutions but also to successfully integrate advanced Pallet Shuttle technology into existing warehouse environments, extending the value and performance of established storage infrastructure.
Engineering Warehouse Throughput
This project demonstrates how existing warehouse infrastructure can be enhanced through intelligent automation rather than complete replacement.
By integrating RF Pallet Shuttle technology into an established high-density storage system, LSE helped improve pallet handling efficiency, optimise warehouse flow and maximise the value of the customer’s existing investment.
Whether supplying complete Pallet Shuttle installations or upgrading existing warehouse systems, Logistics Systems Engineering (LSE) delivers engineered solutions that increase throughput, improve operational efficiency and support long-term warehouse performance.
Project Images & Illustrations
Ask an Expert
I would like a Quote for LSE’s Pallet Shuttle Racking System
Please Fill in the Form Below. Specify the Product Information you Require or How LSE can Help you.